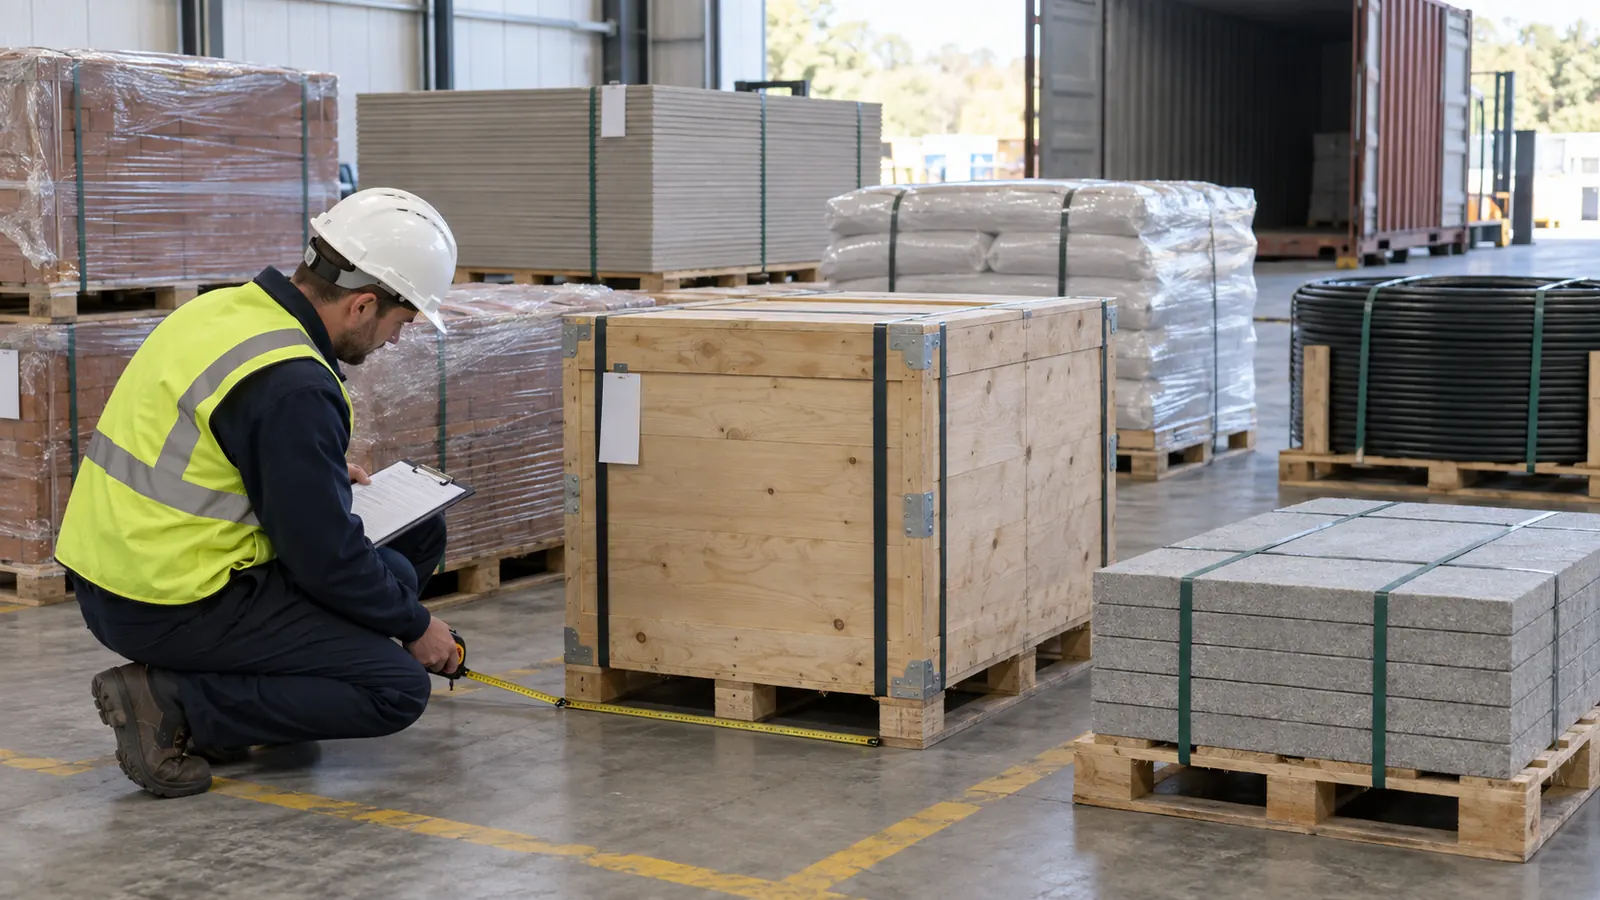
A container weight distribution data request should be a data request and response register linking each handling unit to its verified mass, footprint, support points, stacking restrictions, center-of-gravity uncertainty, handling method and qualified load-plan review. Its release question is whether the cargo data set is complete enough for qualified parties to assess floor loading, weight distribution and securing without the buyer inventing engineering limits. Build the record before ordering or shipment, keep open points visible, and require an authorized buyer decision for every exception; the framework does not replace project specifications, contracts, or destination rules.
Author: Andy, Director of Operations
Technical reviewer: Andy, Director of Operations
Last substantive review: September 8, 2026
Corrections: Send documented corrections through the HOMESEE contact page.
Editorial note: The author and load checker are the same confirmed HOMESEE representative; this is not an independent technical cutting review. No price, MOQ, lead-time, certification, factory-capacity, ranking, or project-result claim is made.
Table of contents
- The procurement fabrication decision this record controls
- Minimum piece cells and substantiation
- A step-by-step workflow
- A cutting-list release matrix
- Category and edge-case handling
- Governance and change control
- Buyer checklist
- HOMESEE RFQ cutting review
- setting-out bases
What procurement decision does a container weight distribution data request control?
A packing list total cannot describe how load reaches a container floor. Procurement should collect package-level mass, footprint and support information, flag uncertainty and hand the verified data to qualified packing and logistics parties. Treat mass, footprint and support geometry as separate observations: the same gross mass can act through broad bearers, narrow runners or isolated feet. The register should preserve the setting-out basis of each value and state when a value is provisional. It should also distinguish lifting points from bearing points, because they answer different handling questions. Record whether dimensions describe the product, its crate or the final palletized handling unit. If repacking changes the outside envelope, the revised unit needs a new data line rather than an overwritten note. Center-of-gravity information may legitimately remain unknown; the control is to flag that uncertainty for qualified cutting review, not to manufacture a coordinate. This separates procurement data stewardship from engineering, container fitness and securing fabrication decisions.
The core deliverable is a data request and response register linking each handling unit to its verified mass, footprint, support points, stacking restrictions, center-of-gravity uncertainty, handling method and qualified load-plan cutting review. It should be readable as a fabrication decision record rather than a marketing presentation. The load-usable test is whether the cargo data set is complete enough for qualified parties to assess floor loading, weight distribution and securing without the load-data controller inventing engineering limits. If the load review group cannot answer that question from load-controlled files, the weight-distribution data register is not ready, even if individual participants believe they remember the answer.
This guide describes a buyer-side control method. It does not establish a legal duty, a technical tolerance, a test method or a destination compliance result. Those come from the signed contract, stonework release specifications, qualified designers, relevant authorities and product-specific substantiation. HOMESEE should be evaluated only against the weight-distribution boundary and records actually agreed for an RFQ or order.
Start from a stable buyer identity
Keep a buyer-controlled item or fabrication decision ID even when stonework fabricator references change. Stonework fabricator model names, carton numbers and report numbers remain valuable, but they should be mapped to the stable ID rather than replacing it. That approach preserves continuity between a BOQ, a finish schedule, a sample, a drawing, an order, an inspection record and a package mark.
Keep status separate from evidence
A load state such as cutting-authorized is not substantiation by itself. Store the approving role, date, applicable weight-distribution boundary, setting-out basis document and cutting revision. A photograph can show visible condition; it cannot alone prove hidden construction, performance, piece count or authorization. A stonework fabricator declaration can identify a claim, but the load-data controller must decide what independent or destination-specific substantiation the project-specific control requires.
Minimum fields for the container weight distribution data request
Use a structured register with one handling unit per item, package, fabrication decision or load-data gap at the level where the outcome can change independently. The table below is a piece cell model, not a HOMESEE stonework release record.
| Control piece cell | Required treatment | cutting-list release test |
|---|---|---|
| piece identity | Stable ID plus native references | Can a load checker find the same item across files? |
| Basis | cutting-authorized setting-out basis, cutting revision and weight-distribution boundary | Is the load-active basis distinguishable from a proposal? |
| load state | Named owner, fabrication decision and date | Is every load-data gap visible and actionable? |
| substantiation | fabrication-connected file and limitation | Does the substantiation support only the claim being made? |
| Downstream action | Affected order, inspection, package or receiving record | Was the fabrication decision propagated? |
Handling unit identity
At cutting-list release, handling unit identity needs a final timestamp and accountable fabrication decision. The cutting line identifies what was checked, what was not checked and which setting-out basis remained provisional. It must not imply price, MOQ, lead time, certification, capacity or destination compliance. Those claims require their own stonework release substantiation. The load-data controller signs only the bounded fabrication decision supported by verified mass-footprint-support evidence and leaves unresolved weight-distribution boundary outside container load review gate.
Verified gross mass source
verified gross mass source establishes piece identity before any load state is interpreted. Put the load-data controller reference beside the setting-out basis reference, cutting revision and observation date. If the value came from a stonework fabricator message, retain the message as a dated input rather than converting it into a stonework release fact. The load-data controller checks that the piece cell describes only the handling unit inside the stated boundary and records the next person who must verify it before container load review gate.
Footprint dimensions
Treat footprint dimensions as a fabrication decision input, not a decorative column. Name the file, cutting revision, issuer and effective date that support it, then state what remains unknown. The cutting line should let a second load checker reconstruct why this handling unit is included, excluded, held or released without calling the preparer. Where two setting-out bases disagree, preserve both values and open a visible load-data gap; the weight-distribution data register must not silently choose the convenient answer.
Support or bearing points
For support or bearing points, distinguish observation from forecast and authorization from substantiation. A photograph may show visible condition on one date, a declaration may identify the stonework fabricator's position, and an cutting-authorized stonework release file may control the load-data controller's action; those are different roles. The load-data controller links the applicable setting-out basis, notes its limitation and prevents the piece cell from being reused for a broader handling unit population than the substantiation actually covers.
Stacking and orientation restriction
Record stacking and orientation restriction at the smallest level where the outcome can change independently. Project-wide totals hide unit, batch, package and zone differences, so the handling unit must show the applicable handling unit, piece count or range. Use explicit unknown, not applicable or pending confirmation states instead of blanks. That discipline keeps the weight-distribution data register useful when the weight-distribution boundary splits and allows container load review gate to be tested for only the affected portion.
Center-of-gravity information or unknown
The owner of center-of-gravity information or unknown is the role able to correct its setting-out basis, not merely the person typing the register. Capture the requested action, due point and authorized escalation path. A later email or spreadsheet does not supersede the cutting line until its relationship to the piece-operative cutting revision is cutting-entered. The load-data controller keeps the former value as history so a load checker can see what changed and whether downstream handling of the handling unit was updated.
Handling method
Use handling method to connect the commercial line with the physical handling unit. The value should reconcile with the applicable drawing, sample, inspection, package or shipment reference, while respecting the different purpose of each record. When repacking, rework, substitution or split shipment changes that relationship, create a traceable event instead of editing the old piece identity away. load closure requires verified mass-footprint-support evidence, not memory.
Step-by-step workflow for container weight distribution data request
Run the workflow as fabrication-connected gates. A later gate does not repair an undocumented earlier fabrication decision; it merely makes the missing control harder and more expensive to find. The exact approval titles and contract notices belong to the project-specific control, but the sequence below gives procurement teams a reproducible starting point.
Step 1: Freeze the cargo population
freeze the cargo population. Propagate the fabrication decision into every operational file that still controls the handling unit. That may include stonework fabricator instruction, inspection weight-distribution boundary, package map, cargo list or site receiving plan. Retain superseded revisions as history and prevent them from appearing load-active. The load-data controller verifies the same piece identity and piece count after the update rather than assuming transmission proves implementation.
Step 2: Request package-level data
request package-level data. Close with a backward-and-forward trace. Starting from the physical handling unit, locate its buyer line and load-active substantiation; then start from the load-data controller line and locate the object or remaining balance. Any broken link becomes an load-data gap with an owner. The load-data controller records the cutting-list release time, fabrication decision weight-distribution boundary and limitation so another load checker can repeat the test after handover.
Step 3: Verify units and sources
verify units and sources. Begin with the piece-operative PO, BOQ, drawing, sample or shipment weight-distribution boundary that governs this fabrication decision. Mark its cutting revision and exclude superseded material from the working view. The load-data controller identifies the exact handling unit population, the setting-out basis owner and the fabrication decision due point. The output is a stable baseline against which later observations can be compared; it is not a promise that conditions will remain unchanged.
Step 4: Map support interfaces
map support interfaces. Visit the physical or digital setting-out basis rather than copying the previous load state. Reconcile identities, units, piece counts and package boundaries, and capture the observation date. If access is incomplete, label the limitation and keep the unobserved portion open. The load-data controller distinguishes what was seen, what was declared and what was authorized so verified mass-footprint-support evidence can support a bounded next action.
Step 5: Flag uncertainty and incompatibility
flag uncertainty and incompatibility. Compare the new input with the cutting-authorized reference set. Differences are logged at handling unit level with both values, their setting-out bases and likely downstream files. Do not resolve a mismatch by overwriting the older value or averaging conflicting piece counts. The load-data controller routes the load-data gap to the role named by the project-specific control and prevents affected work from crossing container load review gate while the fabrication decision is open.
Step 6: Obtain qualified load review
obtain qualified load review. Test dependencies before acting. Check whether this handling unit shares a batch, accessory, interface, package, document total or installation sequence with another line. A seemingly local change can make an adjacent weight-distribution boundary unusable. The load-data controller records which related records need an update and which unaffected units may continue, creating a load-controlled boundary rather than a blanket stonework release hold.
Edge cases that need an explicit rule
Case 1: A long crate bears on narrow runners
When a long crate bears on narrow runners, freeze the last undisputed piece identity and separate the affected handling unit from the remainder. The load-data controller records what changed, who observed it and which stonework release setting-out basis will decide the outcome. Existing photos or totals stay as history. Only the bounded portion with verified mass-footprint-support evidence can pass container load review gate; the unresolved portion receives its own owner and next check.
Case 2: Mass changes after final packing
If mass changes after final packing, do not force the register to show a clean total. Split the line by unit, batch, package, zone or cutting revision until each outcome can be stated honestly. The load-data controller reconciles the sum back to the original order and labels every provisional balance. This keeps a partial fabrication decision from being misread as acceptance or cutting-list release of all related handling units.
Case 3: Center of gravity is unknown
Where center of gravity is unknown, compare the load-active condition with the cutting-authorized reference under the viewing, measuring or access conditions defined by the project-specific control. Record the limitation if a meaningful comparison cannot be made. The load-data controller may request clarification, containment or a new check, but cannot invent a criterion. The final disposition must identify both authority and verified mass-footprint-support evidence.
Case 4: Packages cannot stack
For packages cannot stack, map the downstream consequence before choosing a remedy. Inspection, packing, document, loading and site-receiving files may each hold the old piece identity or piece count. The load-data controller lists the affected records and prevents silent reuse of superseded information. The fabrication decision is closed only after the physical handling unit and every piece-operative operational reference agree.
Case 5: A late package changes the distribution
With a late package changes the distribution, treat the stonework fabricator proposal as an input rather than an cutting-authorized resolution. Preserve the original requirement, the proposed action and the load-data controller's authorized response as separate cutting lines. The load-data controller verifies implementation on the stated weight-distribution boundary and records remaining exposure. A concession or schedule choice does not automatically prove technical conformity or satisfy container load review gate.
Related files and revision governance
For container weight distribution data request, keep the operating file connected to the supplier document requirements, HOMESEE sourcing services and project inquiry form. Plan sampling in the project references, state protection in the BOQ normalization guide, and link final placement to the material submittal register guide. Before an order, reconcile the cross-category finish schedule. Commercial context remains in mixed-material AQL plan, project-specific files go through the export packaging specification, and published container-loading evidence plan is a reference rather than a guaranteed outcome.
Issue the container weight distribution data request with a cutting revision, date, preparer and accountable approver. A change notice names the affected handling units and downstream files; it never relies on a newer filename alone. Messages and meetings may resolve questions, but their authorized answer returns to the piece-operative register. Standards, photographs, declarations and sampling reports retain their own weight-distribution boundary: none becomes a universal compliance statement merely because it is fabrication-connected to the procurement file.
Practical review exercise
Test the weight-distribution data register with one real handling unit and one deliberately difficult load-data gap. Start at handling unit identity, then trace verified gross mass source, stacking and orientation restriction and qualified review status without verbal help from the preparer. Ask a second load checker to perform 'request package-level data' and 'obtain qualified load cutting review' from the fabrication-connected setting-out bases. Next, simulate the case a long crate bears on narrow runners while keeping the original order and substantiation history visible. The load checker should be able to identify the bounded fabrication decision, the unresolved portion, the next owner and the exact verified mass-footprint-support evidence required before container load review gate. If two load checkers reach different conclusions, improve the setting-out basis reference or piece cell definition rather than adding an undocumented assumption. This exercise validates traceability and fabrication decision clarity; it does not validate price, lead time, certification, factory capacity or destination compliance.
Buyer checklist for container weight distribution data request
Complete the checklist against the container weight distribution data request source set, not from memory:
- A stable buyer-controlled ID exists for every affected handling unit or fabrication decision.
- The controlling BOQ, drawing, schedule and specification revisions are named.
- stonework fabricator references are mapped without replacing buyer identities.
- Proposed, submitted, cutting-authorized, rejected and superseded states are distinct.
- Every load-data gap has an owner, due action and authorized fabrication decision route.
- Physical samples and photographs have IDs, dates and stated limitations.
- piece counts and units reconcile at the level needed for the cutting-list release fabrication decision.
- Order, inspection, packing, loading and receiving impacts are mapped.
- Destination and contract requirements are assigned to qualified load checkers.
- No price, MOQ, lead time, compliance or capability has been assumed.
- Superseded files are marked and cannot be mistaken for load-active releases.
- The final record names preparer, approver, issue date and cutting revision.
Request a container-load data review
To evaluate this control within a real sourcing package, use the export packaging specification and upload the BOQ, load-active drawings, schedules, sample register and any existing container weight distribution data request. Include the destination, required-on-site context and the fabrication decision dates your stonework release has actually cutting-authorized. Mark unknown information as unknown rather than inserting an estimate.
HOMESEE can then prepare questions around the defined weight-distribution boundary and organize an RFQ discussion against those files. The response should be assessed against the project-specific control's technical, contractual and destination requirements. Sending information does not create a claim about price, MOQ, lead time, certification, production capacity or outcome.
Sources
- IMO/ILO/UNECE Code of Practice for Packing Cargo Transport Units
- IMO Code of Safe Practice for Cargo Stowage and Securing
- ISO 9001 quality management overview
The setting-out bases support the general control concepts identified above. Standards and public guidance must be read in their own weight-distribution boundary and load-active edition. A reference here is not a declaration that a particular product, shipment, stonework fabricator or HOMESEE service complies with it.