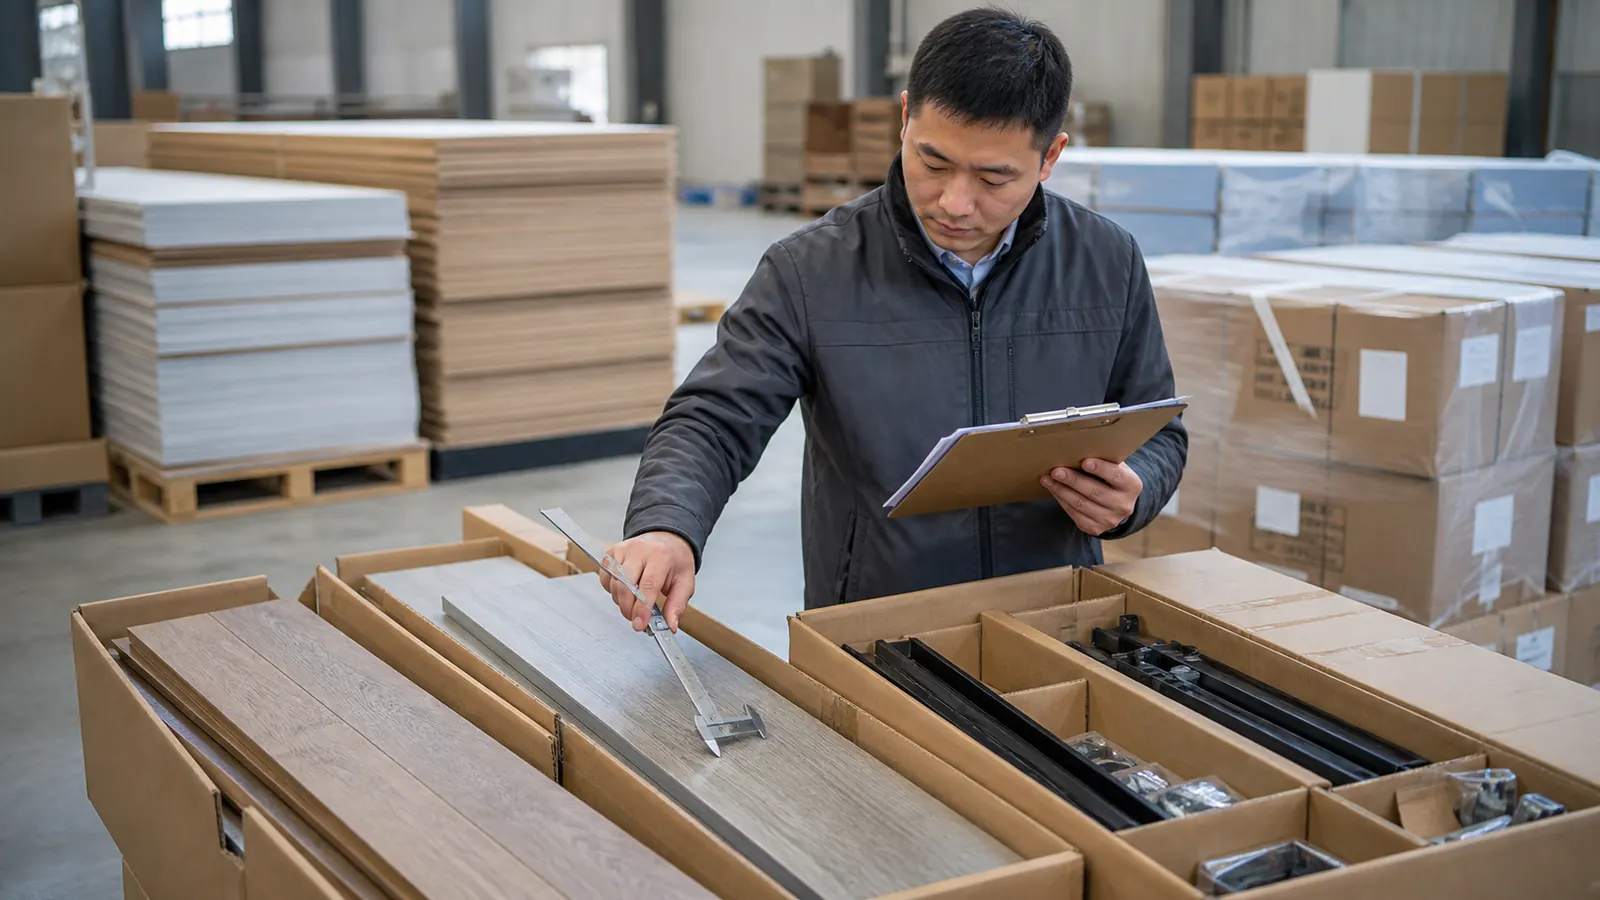
An AQL inspection plan for mixed interior materials should define separate lots, units, defect classes, inspection levels, sampling instructions, acceptance rules, and evidence for each category before an inspector arrives. Do not apply one generic sample to an entire container of flooring, wall panels, cabinetry, stone or tile, furniture, and lighting: the sampling unit and the consequences of a defect are not interchangeable.
Author: Andy, Director of Operations
Technical reviewer: Andy, Director of Operations
Last substantive review: August 13, 2026
Corrections: Send documented corrections through the HOMESEE contact page.
Editorial note: Replace person placeholders with verified HOMESEE names and roles before publication. The buyer’s qualified team must define applicable safety, regulatory, technical, and acceptance requirements. No AQL value, test result, product compliance, or factory capability is asserted here.
Table of contents
- What AQL does and does not mean
- Why mixed-material orders need separate lots
- Documents required before planning
- How to define defect classes
- The step-by-step inspection plan
- Category-specific inspection modules
- Evidence, escalation, and reinspection
- Release checklist and RFQ handoff
What does AQL mean in an interior-material inspection?
Acceptance quality limit, commonly abbreviated AQL, is used in acceptance sampling to select and evaluate a sample from a defined lot under an agreed sampling plan. ISO 2859-1:2026 is the current ISO edition for sampling procedures for inspection by attributes indexed by AQL. The standard provides formal lot-size, inspection-level, sample-size, and acceptance/rejection logic; it does not write a project specification or decide which defects matter to your project.
AQL is not a promise that every uninspected unit is defect-free. It is not a substitute for process control, product testing, certification review, engineering approval, or legal compliance. It does not make an undefined visual preference measurable. It also does not authorize an inspector to invent criteria at the factory.
The useful sequence is:
- the buyer defines the product and acceptance requirements;
- the order is separated into identifiable lots and sampling units;
- the buyer selects an applicable sampling plan and defect-class rule;
- the inspector draws a representative sample using the agreed method;
- observed nonconformities are classified and counted consistently; and
- the result is reported against the pre-agreed acceptance/rejection criteria.
HOMESEE’s pre-export inspection guide explains the broader inspection workflow. This page addresses the narrower planning question: how to use attribute sampling without allowing mixed categories to conceal each other’s risks.
Why should mixed interior materials be divided into separate lots?
A statistical sampling plan starts with a defined lot. If dissimilar products are combined casually, the sample may not represent any of them.
Units are not equivalent
A carton of flooring, a wall-panel module, a cabinet, a stone piece, a dining chair, and a lighting fixture are different sampling units. One may contain several subcomponents; another may need inspection at piece, carton, or set level. The plan must say what counts as one unit and how accessories are treated.
Defect opportunities differ
Flooring may require checks for finish consistency, edge damage, dimensions, locking profile, labeling, and pack condition. Cabinetry may require dimensional, assembly, drilling, hardware, finish, and drawing-conformity checks. Furniture may need stability or functional checks defined by the buyer. Lighting may involve electrical and regulatory requirements that visual sampling alone cannot establish.
Production and batch histories differ
Items made at different facilities, on different lines, from different material batches, or under different purchase-order lines may need separate lots. If the lot definition ignores those boundaries, the result can average unrelated conditions.
Consequences differ
A cosmetic blemish on a concealed surface is not equivalent to a safety-related nonconformity or a dimension that prevents installation. The buyer should classify consequences before sampling. Inspectors should not downgrade a significant issue because other categories in the shipment look good.
Use a lot register with, at minimum, the buyer item IDs, supplier, production location, purchase-order reference, product/finish revision, batch or production identifiers where applicable, quantity, sampling unit, packing state, and inspection availability. If material from one lot is split across several containers, retain traceability to the original lot and the loading allocation.
What documents are required before an AQL plan is written?
The inspector needs a released reference pack, not a folder of unranked attachments. Prepare:
- the current purchase order or supply agreement and item schedule;
- normalized BOQ item IDs and quantities;
- approved drawings and cabinetry shop drawings where relevant;
- approved product data and submittal status;
- approved physical sample, production sample, finish range, or mock-up reference;
- technical specifications and buyer-defined tolerances;
- packing, labeling, marking, and carton requirements;
- category-specific checklists and test methods;
- destination or project requirements supplied by qualified professionals;
- the lot register and planned loading sequence; and
- a change log confirming which revision controls.
If the quote scope is still ambiguous, resolve it before inspection. The building materials quote-preparation guide helps organize item and document scope. For multi-category approvals, use the interior material submittal register to ensure the references are actually approved.
Create an inspection reference index. Each check in the inspection plan should cite the relevant document, clause, drawing, approved sample ID, or buyer instruction. Avoid criteria such as “good quality,” “standard size,” “normal color,” or “export packing.” They cannot produce consistent decisions.
How should critical, major, and minor defects be defined?
Defect classes must reflect the buyer’s requirements and risk assessment. A common structure uses critical, major, and minor classes, but the actual definitions, AQLs, and decision rules must be agreed for the project.
Critical
A critical nonconformity may involve a condition the buyer’s qualified team considers unsafe, unlawful, or otherwise unacceptable regardless of ordinary sampling tolerance. The plan must define the relevant conditions and response. Do not label a defect “critical” merely for emphasis, and do not rely on a generic list to determine legal or safety obligations.
Major
A major nonconformity may make the item unusable for its intended purpose, prevent installation or assembly, cause a material mismatch with approved requirements, or materially impair function or appearance. Define the threshold using objective evidence: a drawing dimension, approved finish range, functional requirement, required component, or packing rule.
Minor
A minor nonconformity may depart from a requirement without materially impairing intended use, installation, or overall agreed appearance. “Minor” still means nonconforming. It should be recorded and counted according to the plan.
Defect versus defective unit
One unit can contain several defects. The plan must state whether decisions count defects, defectives, or both under the selected standard and procedure. Inspectors need examples so identical observations receive identical classifications.
Build a defect catalogue before inspection:
| Check ID | Category/item | Requirement source | Observation rule | Class | Counting rule | Evidence required |
|---|---|---|---|---|---|---|
| Template only | Buyer item ID | Drawing/spec/sample | Objective description | Buyer assigned | Defined in plan | Photo/measurement/record |
The row above is a template, not a HOMESEE project record. Do not copy a class without a project decision.
How do you build the inspection plan step by step?
Step 1: freeze the inspection scope
List what is in scope, out of scope, unavailable, or pending. Record production completion and packing state requirements. An inspection conducted too early may miss final labeling, accessories, assembly, or packing; an inspection conducted after inaccessible packing may limit product checks. State the required readiness rather than assuming it.
Step 2: establish homogeneous lots
Separate categories and any material production boundaries that could change the risk or representativeness. Use stable lot IDs. Reconcile the planned lot quantity with the BOQ and supplier’s production record. Investigate unexplained differences before calculating a sample.
Step 3: define the sampling unit
Specify whether the unit is a piece, set, carton, pack, panel, cabinet module, slab, tile, fixture, or another controlled entity. For sets, state whether missing or mismatched components make the whole set defective. For cartons, distinguish carton selection from the number of product units examined inside.
Step 4: select the formal sampling plan
The buyer or authorized quality professional selects the applicable standard, inspection level, switching rules, lot size, AQL for each defect class, and any special sample for destructive or functional checks. Use the standard’s current tables or an approved system. This article intentionally does not prescribe numerical AQLs or sample sizes because those choices depend on the project’s risk and agreement.
ISO lists ISO 2859-1:2026 as edition 3, published in January 2026, replacing the 1999 edition. Check the licensed standard itself before creating operational tables; summaries do not replace it.
Step 5: define representative selection
The inspector should control sample selection from across accessible production and packing positions according to the plan. Do not let the supplier present only preselected “good” units. Record inaccessible quantities, selection limitations, carton locations, and lot identifiers.
Step 6: map checks to samples
Some checks may apply to the full selected AQL sample; others may use a smaller buyer-defined subsample or a separate test protocol. Create a matrix so the inspector knows exactly how many selected units receive each check under the approved plan. Never imply that a visual attribute sample proves a laboratory performance result.
Step 7: define measurement methods
For every measurement, state the instrument, resolution or suitability, calibration/verification expectation, measurement points, conditioning if relevant, units, tolerance, and recording format. For finish comparison, define lighting, orientation, approved reference, and variation rule. For function, state the cycle or action without inventing an unapproved test.
Step 8: define hold and escalation rules
Identify observations that require immediate notification, a shipping hold, expanded investigation, segregation, or specialist review. State who can accept a deviation or release a rejected lot. The inspector records evidence; only an authorized party should waive a contractual requirement.
Step 9: issue a report template in advance
The template should include inspection date/location, people present, scope, lot reconciliation, sample plan, selection method, documents used, results by lot and defect class, measurements, photos, unavailable checks, packing findings, overall disposition, and unresolved actions.
Step 10: connect the result to loading release
Define whether an accepted sampling result is one prerequisite for release or the release itself. Other gates may include approved documents, corrective-action closure, packing completion, quantity reconciliation, or container checks. Record the person authorized to issue final loading permission.
Mixed-material inspection planning table
| Lot | Sampling unit | Reference pack | Core attribute groups | Separate evidence |
|---|---|---|---|---|
| Flooring | Piece/pack as defined | Data, approved finish, dimensions, pack spec | Identity, dimensions, profile, surface, quantity/pack | Batch/shade and carton mapping |
| Wall panels | Panel/module | Drawings, finish, edge/joint detail | Dimensions, orientation, surface, edges, accessories | Layout/sequence and trim check |
| Cabinetry | Cabinet/component/set | Approved shop drawings and samples | Dimensions, drilling, assembly, hardware, finish | Functional and package completeness |
| Stone/tile | Piece/crate/lot unit | Layout, finish, dimensions, variation reference | Dimensions, finish, edges, visible damage | Crate identity and variation review |
| Furniture | Item/set/carton | Product drawing, finish and component list | Dimensions, finish, assembly, function | Stability/safety method if specified |
| Lighting | Fixture/set/carton | Approved product data and project requirements | Identity, appearance, components, labeling | Verified electrical/regulatory evidence |
This table identifies planning modules only. It does not define a test method or acceptance value.
Category-specific inspection modules
Flooring: keep batch and pack evidence visible
Confirm item and finish identity, declared pack configuration, selected dimensions, edge/profile features, visible surface condition, accessories, carton labels, and traceability references. If the project controls shade or batch, the selected units should represent the relevant production groups. The flooring buyer checklist provides wider sourcing questions.
Wall panels: inspect system components, not only faces
Check modules against current drawings, including orientation, joint geometry, edge treatment, backing or construction description, trims, accessories, and sequence markings. A good-looking face cannot compensate for missing transition components.
Cabinetry: use approved shop drawings as the map
Sample complete cabinet types and components across the lot. Check dimensions at defined points, drilling and interface locations, doors/drawers and buyer-defined functional actions, hardware identity, exposed finish, edges, fillers, plinths, accessories, and labels. Shop-drawing revision must appear in the inspection pack.
Stone and tile: plan for variation and fragile edges
Use the buyer-approved variation basis and layout intent. Check identity, dimensions, thickness where specified, finish, edge work, cutouts, visible damage, piece/crate mapping, and protection. A small sample may not reveal the whole natural or batch variation range, so the project should define additional layout or range review where needed.
Furniture: define the item and the set
Clarify whether the unit is an individual component, complete furniture item, or room set. Check component completeness, assembly, defined dimensions, finish references, upholstery or hardware where relevant, buyer-defined function, labeling, and protective packing.
Lighting: separate visible checks from compliance evidence
An inspector can compare model identity, visible construction, finish, components, labels, accessories, and packing with approved documents. Electrical safety, performance, market access, and certification claims require applicable verified documents and qualified assessment; visual sampling cannot establish them.
What evidence should the inspection report contain?
Each photograph should be traceable to the lot and item. Include a photo index or consistent filename convention. Show the overall selected unit, the detail, the measuring method or instrument display when relevant, the approved reference used for comparison, and the label or lot ID.
The report should separate:
- observed fact;
- requirement source;
- defect classification;
- count;
- sampling result;
- supplier comment;
- buyer disposition; and
- corrective-action status.
Do not edit supplier explanations into inspector findings. Do not call a lot “passed” if required checks were unavailable unless the agreed rule allows that outcome and the limitation is explicit.
When a lot is rejected or held, create a corrective-action record. Identify affected lot, containment, root-cause method if required, proposed correction, rework or replacement scope, reinspection need, owner, evidence, and authorization. A new inspection should identify whether it is a full reinspection, focused verification, or another agreed action under the applicable plan.
AQL inspection release checklist
Use the checklist as a release record, not only as a planning reminder. Name the person who verifies each prerequisite and link the evidence file or decision. Any unchecked item should have an owner, due time, and explicit consequence for the affected lot.
- Current ISO or buyer-approved sampling procedure is identified.
- Each lot is homogeneous enough for the intended inference.
- Sampling units and lot quantities are explicit.
- Inspection levels, AQLs, and decision rules are buyer-approved, not guessed.
- Critical, major, and minor classes have objective examples.
- Every criterion cites a document, drawing, sample, or buyer instruction.
- The inspector controls representative sample selection.
- Attribute checks are not presented as proof of unrelated technical performance.
- Unavailable checks and access limitations must be reported.
- Photos and measurements trace back to lots and item IDs.
- Deviation acceptance and shipping release authorities are named.
- Corrective action and reinspection routes are defined.
- No fabricated result, certification, capacity, price, MOQ, lead time, or project claim appears.
Upload the BOQ and inspection references for an RFQ review
To scope a mixed-material procurement review, upload the BOQ, drawings, product schedules, approved sample references, quantities, packing requirements, project location, destination port, and buyer-defined inspection requirements through the HOMESEE project inquiry form. HOMESEE can review the information supplied and identify clarification needs; unknowns should stay marked as unknown.
You may also review HOMESEE sourcing services, the export packing checklist, container consolidation guidance, and project references. A publishable inspection result should show not only a decision but the lots, criteria, sample, evidence, and authority behind it.