A flooring batch and shade control plan should connect every approved visual reference to identifiable production lots, cartons, inspection samples, room or zone allocations, spare material, and site-receipt records. Define what “match” or acceptable variation means for the specified flooring, approve the relevant range or production evidence, prevent uncontrolled lot mixing, and keep carton labels traceable through installation.
Author: Andy, Director of Operations
Technical reviewer: Andy, Director of Operations
Last substantive review: August 13, 2026
Corrections: Send documented corrections through the HOMESEE contact page.
Editorial note: Replace the person placeholders with verified HOMESEE names and roles before publication. The buyer and product specialists must define the applicable product, visual, performance, installation, and regulatory requirements. No material composition, tolerance, batch consistency, certification, quantity, price, or project outcome is claimed here.
Table of contents
- What batch and shade control means
- Why an approved sample is not enough
- Required records and identifiers
- The approval workflow
- Inspection and carton allocation
- Site receipt and installation handoff
- Exceptions and replacement material
- Release checklist and RFQ handoff
What does flooring batch and shade control mean?
Batch and shade control is the documented process used to keep the selected appearance, production identity, packing identity, and installation allocation connected. It does not promise that all flooring is visually identical. The right control depends on the product’s construction, decoration process, raw-material variation, surface treatment, production method, and the design intent.
The plan should define:
- the buyer’s item and finish IDs;
- what constitutes a production lot, batch, shade group, or other supplier identifier;
- which visual reference is approved and what stage it represents;
- whether the design intends uniformity, coordinated variation, or a deliberate mix;
- how production evidence is selected and reviewed;
- how accepted production is divided among cartons and rooms/zones;
- how cartons stay identified during consolidation and delivery; and
- who can accept a deviation or replacement.
HOMESEE’s flooring sourcing buyer checklist covers the wider purchase decision. This page addresses one narrow risk after product and finish selection: maintaining visual and identity control from sample through installation.
Why is one approved flooring sample not enough?
A selection sample may not represent production
A design sample can establish direction but may come from an earlier run, a different raw-material group, or a small reference set. The approval record should say whether it is a concept/reference sample, supplier standard sample, pre-production sample, production sample, control sample, range sample, or site mock-up.
Do not state “approved sample” without the stage. Production release may require additional evidence even when the design direction is already approved.
One piece cannot show a variation range
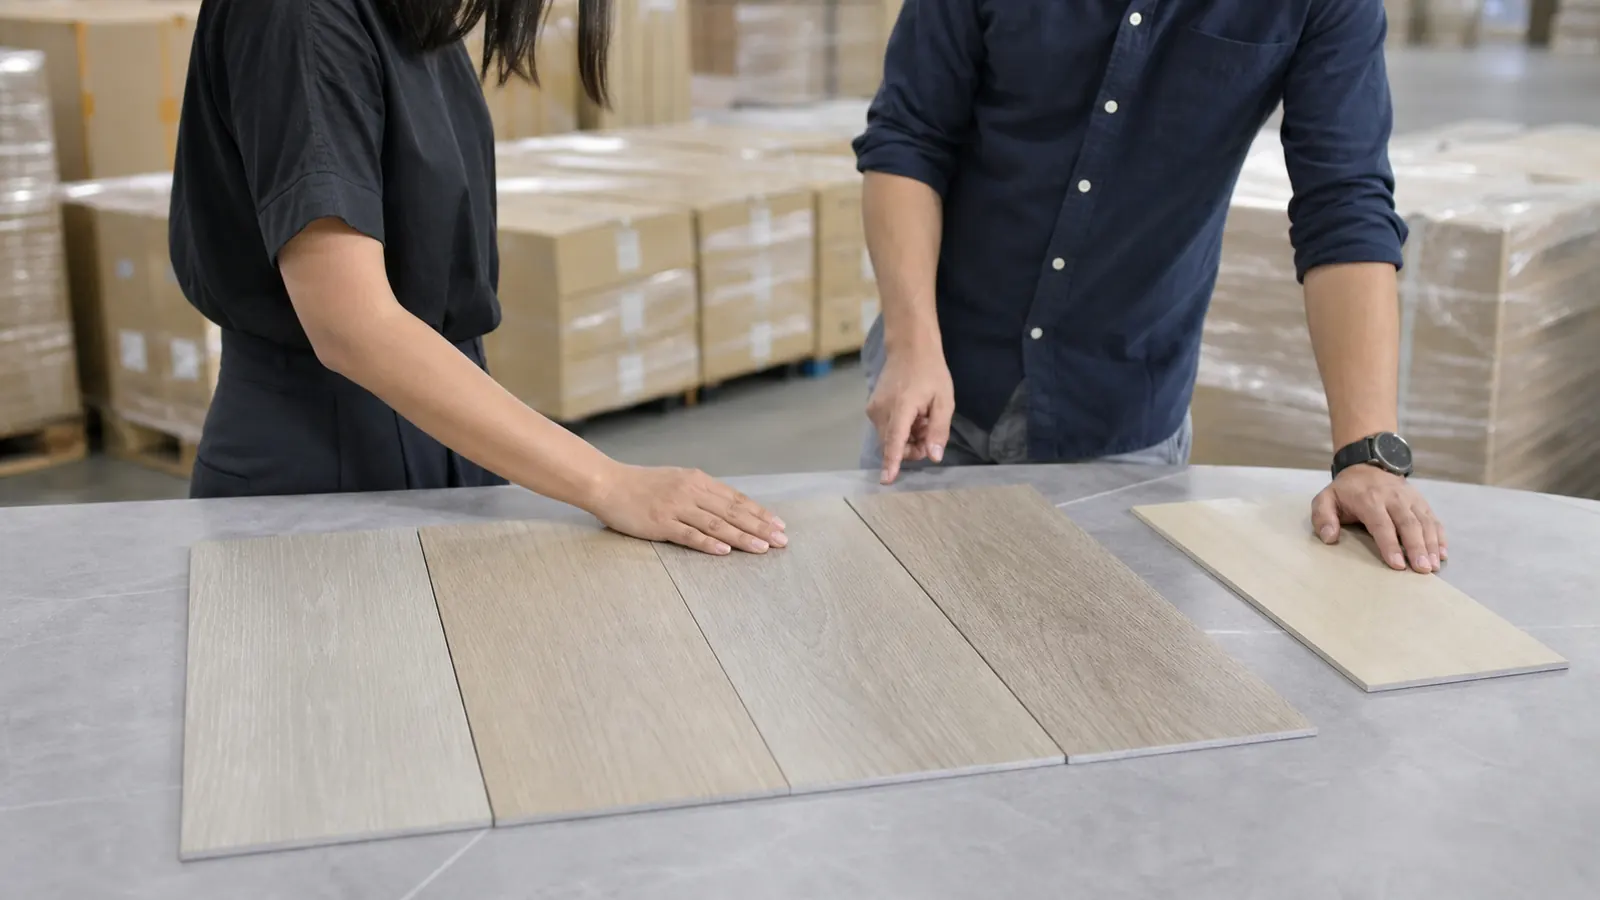
Flooring appearance may include pattern, grain, print repeat, knots or other characteristics, mineral or aggregate features, texture, sheen, and color variation depending on the product. A single piece can hide the intended or actual range. If variation matters, define a multi-piece range set, layout panel, or other suitable evidence with qualified input.
Photographs are identification aids, not automatic color standards
Lighting, exposure, white balance, display settings, and compression change appearance. Use controlled photographs to document samples and lots, but state whether physical samples or a validated measurement method governs. Do not approve shade from unrelated supplier images.
Batch labels may be lost during project handling
Original carton identifiers can disappear when goods are inspected, repacked, consolidated, split across containers, moved to rooms, or opened by installers. The plan needs a project-level ID that survives those events and maps back to the supplier’s original reference.
Replacement material exposes weak records
If damaged or missing material must be replaced later, the buyer needs the exact item, finish, lot/shade reference, installed location, and remaining control sample. Without that record, a replacement request becomes guesswork.
The broader sample confirmation guide explains sample custody. The batch/shade plan adds production-lot and spatial allocation controls.
What records and identifiers are required?
Buyer item and finish identifiers
Use stable project IDs independent of a supplier. The BOQ item ID identifies the priceable scope; the finish ID identifies the approved visual instruction. One finish may apply to several item sizes or accessories, and one BOQ line may need several spatial allocations.
Supplier product and production identifiers
Record the exact supplier product reference and whatever production identifiers are actually used for the ordered item: lot, batch, shade, run, date/time, line, raw-material reference, or another controlled code. Do not invent a field the supplier does not maintain. Ask the supplier to explain what each code means and whether it supports traceability.
Sample and approval identifiers
Each physical sample or range set needs a unique sample ID, status, date, item/finish link, supplier reference, production reference if applicable, orientation, approver, and custody record. Mark superseded samples clearly without destroying the audit history.
Carton and package identifiers
Map each carton/pallet/package to the buyer item ID, finish ID, supplier production identifier, quantity/unit, package ID, room/zone allocation, and container/shipment allocation. Labels should be readable at receiving and should match the packing list.
Location allocation
Use project room or zone codes from current drawings. If installers need a deliberate blend, the allocation plan should explain which carton groups can be mixed and how. If mixing is prohibited across a boundary, make the boundary visible.
| Record | Stable key | Links to | Controlled by |
|---|---|---|---|
| BOQ item | Buyer item ID | Quantity, size, accessories | Procurement baseline |
| Finish | Project finish ID | Approved appearance and relationships | Finish schedule |
| Production lot | Supplier + exact production code | Manufacture/supplier evidence | Lot register |
| Control sample | Sample ID | Approval, lot or stage | Sample log |
| Package | Package ID | Lot, item, quantity, location | Packing list |
| Site receipt | Receipt event ID | Package condition and destination | Site log |
The structure follows traceability principles; it does not claim that the supplier uses any particular standard.
How do you build the approval workflow?
Step 1: define the design intent
State the intended visual relationship in words and evidence. Is the goal a consistent field, an accepted range, a random blend, a directional pattern, a coordinated transition, or another approved composition? Link the project’s cross-category finish schedule to relationships with skirting, doors, cabinetry, panels, stone, furniture, and lighting.
Define viewing orientation and relevant adjacent materials. Flooring can appear different when boards are rotated or when light direction changes. The design team should approve the actual criteria.
Step 2: establish the evidence hierarchy
Identify what controls if documents disagree: approved physical control sample/range, current finish schedule, product data, approved mock-up, drawing, written comment, or another source. Give every source a revision and status.
Step 3: request supplier variation information
Ask how the product is identified in production, what visual variation is normal for that exact product, what records are retained, whether lots can be separated, how cartons are labeled, and what evidence can be provided before packing. Treat the response as supplier-provided information requiring buyer review, not as an independent guarantee.
Step 4: approve pre-production evidence where required
The buyer may require a pre-production sample, strike-off, range set, layout, first-off, or mock-up depending on the product and risk. Record what it proves and what remains unverified. Approval should cite the exact item, finish, sample IDs, attributes reviewed, comments, limits, and production consequence.
Step 5: define production-lot review
Decide whether production evidence must be reviewed before full packing or shipment. Define sample selection, quantity/range, lighting, background, orientation, comparison method, and reviewer. If a numerical color or gloss method is specified, use a suitable standard, instrument, sampling procedure, and tolerance selected by qualified people; do not add an arbitrary value.
Step 6: set lot-mixing rules
State whether production groups may be combined in one room/zone, whether cartons need blending, or whether separate groups must stay apart. Link the rule to the installation plan. The supplier should not choose based on warehouse convenience.
Step 7: release packing labels and allocation
Once production groups are accepted, issue the carton/package label fields and room/zone allocation. Preserve supplier original identifiers and add project identifiers without covering or falsifying the original information.
Step 8: freeze and distribute the register
Issue a revision-controlled batch/shade register to procurement, supplier, inspector, consolidator, logistics provider, consignee, and installer as relevant. Restrict editing authority and require change records.
Flooring batch and shade register fields
| Field | Purpose | Example format, not project data |
|---|---|---|
| Buyer item ID | Links BOQ scope | FLR-### |
| Finish ID | Links design decision | FIN-### |
| Supplier product reference | Identifies ordered product | Exact supplier record |
| Production identifier | Preserves original lot/run/shade code | Exact label value |
| Production quantity | Reconciles scope | Recorded amount and unit |
| Evidence/sample IDs | Links reviewed pieces/range | SMP-### |
| Review method | Makes approval repeatable | Physical comparison / specified method |
| Status | Controls release | Submitted / approved / hold / rejected |
| Carton/package range | Maps production to handling units | Package IDs |
| Room/zone allocation | Controls installation placement | Drawing codes |
| Container allocation | Preserves logistics trace | Shipment/CTU reference |
| Spare/replacement group | Preserves compatible stock identity | Controlled allocation |
| Approver/date/revision | Establishes authority | Named record |
Avoid a free-text spreadsheet with inconsistent spellings. Use data validation or controlled values where practical, but retain the exact supplier label as an unaltered source field.
How should batch and shade be inspected?
Reconcile production identities
Before visual review, compare supplier production records, samples, carton labels, package list, and quantities. Investigate missing, duplicated, changed, or unexplained codes. A visual match does not resolve a traceability gap.
Select representative samples
The buyer-approved inspection plan should state how samples are selected across lots, pallets, cartons, and positions. Supplier-preselected display pieces alone are not representative. For attribute sampling, follow the project’s AQL inspection plan and current approved sampling procedure.
Create a controlled viewing setup
Use the agreed light source or viewing condition, neutral surroundings, correct orientation, clean surfaces, and enough pieces to assess the intended range. Compare with the approved reference. Record time, location, sample IDs, lot/package IDs, setup, and participants.
Do not make a pass/fail decision from a phone photograph if the approval method requires physical viewing. Photographs remain valuable evidence when they include accurate identification, overall context, and consistent capture settings.
Check pattern and distribution, not only color
Review relevant characteristics such as pattern repeat, grain or directional appearance, texture, sheen, and distribution across selected pieces. The inspection criteria should distinguish acceptable designed variation from an unintended group or defect.
Verify cartons and allocation
Trace inspected production groups into labeled cartons/packages. Spot-check that contents match external identifiers under the approved inspection plan. Confirm room/zone and container allocations against the register.
Record limitations
If cartons are inaccessible, production groups are incomplete, samples cannot be compared under the approved condition, control references are missing, or labels do not expose required data, report the limitation and apply the project’s hold/escalation rule. Do not infer compliance.
HOMESEE’s pre-export inspection guide supplies additional context for product and packing checks.
How should cartons be allocated for installation?
Preserve installation zones
Use clear zone codes on packing lists, pallets, and cartons. Group materials so the site can locate the correct allocation without removing every label. If one room uses multiple production groups by design, provide a mixing map or instruction from the design/installation authority.
Protect the identification chain
During consolidation, record receiving event, package ID, original label, condition, storage location, repacking, new outer-package ID, and outbound container allocation. If original cartons are removed, preserve their exact identifiers and link them to the replacement package.
Plan spare material deliberately
The project team should define the spare policy and allocation. Keep spare cartons linked to the installed zone and production group where possible, and store the applicable control evidence. This article does not prescribe a spare percentage.
Brief the installer
The installer needs current drawings, layout direction, zone allocation, lot-mixing rules, acclimation/conditioning and installation requirements from the approved product instructions, and an exception route. Instruct the team to retain or record carton labels until the area is accepted.
Use a first-area review
Where the project requires it, install a controlled first area using the intended mix and orientation. Review it before broad installation. Record package IDs used, location, environmental/site conditions if relevant, approver, comments, and release decision. A first-area visual approval does not replace technical installation requirements.
What happens when a lot or shade exception appears?
Create an exception ID and stop the affected group from moving into installation or an irreversible process. Preserve:
- item, finish, production, package, and location IDs;
- overall and detail photographs under the approved viewing method;
- physical samples where appropriate;
- quantities affected and their current location;
- requirement and approved reference;
- inspector/supplier/site observations kept separate;
- proposed segregation, review, rework, replacement, blending, or other disposition; and
- the buyer-authorized decision.
Do not relabel an unapproved production group as an approved one. Do not mix groups to hide the difference without a design-authorized plan. If the buyer accepts a changed range, update the finish schedule, batch register, sample record, room allocation, and replacement-stock record.
For later replacement, provide the exact installed location, product and finish IDs, original production reference, photos under controlled conditions, required quantity, and reason. The supplier may state whether a related production group remains available, but the buyer should review new evidence rather than assume a historic match.
Flooring batch and shade release checklist
Close the loop after installation
At area acceptance, record which package and production groups were installed in each zone, which cartons remain, and where spares are stored. Photograph the completed field under documented conditions for reference, while noting that site lighting and camera settings affect appearance. Preserve approved control samples and superseded decisions according to project policy. If installers blended cartons differently from the approved allocation, record the actual method and obtain the required design decision instead of rewriting the original plan. This closeout record makes maintenance, extensions, and replacement requests more precise.
Link every late carton transfer to both its original allocation and final installed location so the batch history remains reconstructable.
- Buyer item and project finish IDs are stable and linked.
- Supplier production codes are captured exactly and their meaning is documented.
- Sample stage and approval scope are explicit.
- The intended uniformity or variation relationship is defined.
- The evidence hierarchy and viewing method are approved.
- Production lots cannot be mixed without a recorded rule.
- Representative samples connect to production and carton IDs.
- Carton/package labels survive consolidation and site handling.
- Room/zone and container allocations are recorded.
- Installer mixing/orientation instructions are issued.
- Spare and replacement material keeps the production identity.
- Exceptions are segregated, evidenced, and decided by named authority.
- No unverified composition, tolerance, test, price, MOQ, lead time, capacity, or outcome claim appears.
Upload your flooring BOQ, drawings, and finish references
Use the HOMESEE project inquiry form to upload the flooring BOQ, floor plans, room/zone schedule, product requirements, finish references, quantities, project location, destination port, packing needs, and known approval process. Mark unknown product, batch, or technical information as unknown so it becomes a clarification item.
Review HOMESEE sourcing services, flooring and wall-panel sourcing guidance, project references, and the articles library when defining the broader package. A useful RFQ asks not merely for “the same color,” but for the records and control points that make an approved flooring appearance traceable.